How ADC and DAC Modules Work in Industrial PLC Systems
Analog to digital and digital to analog converters connect real machines.
An adc for industrial plc changes physical signals to numbers. Your plc reads this digital input data in code.
Next, a dac turns numbers into an analog output signal. This signal moves process valves.
You must learn how signals change and map to registers. You need scaling math, quantization limits, and sensor calibration.
Advanced i/o modules help this big market grow:
| Metric | Details |
|---|---|
| 2025 Market Valuation | USD 1.2 billion |
| 2034 Projected Valuation | USD 2.5 billion |
| Anticipated CAGR (2026–2034) | 9.2% |
These parts help input signals in modern automated factories.
Key Takeaways
-
ADC parts change real world signals into PLC digital numbers.
-
DAC parts turn PLC numbers into smooth signals to control machines.
-
The 4-20mA current loops block factory noise best over long distances.
-
PLCs use easy math to change sensor numbers into real units.
-
Regular calibration keeps sensors accurate and stops heat drift errors.
How ADC for Industrial PLC Systems Converts Signals
Factory machines need steady body measures. You use an adc for industrial plc here. It turns real facts into numbers. An analog input module handles these measures. It works in short, neat steps.
Analog Input Signal Sampling and Quantization
Your work starts with sensors. They feel nearby space conditions. Tools like PT100 RTDs read heat. Sensors track push force and fluid flow. The system has three plain steps. It changes real power to digital bits:
-
Field devices change outer facts into current loops.
-
The PLC input part catches this new signal.
-
The built-in ADC reads the steady signal. It maps facts into digital bit counts.
Technical Tip: Inside parts clear quick noise using special filters. Next, sample-and-hold parts stop changing voltage. Finally, registers check the main voltage step.
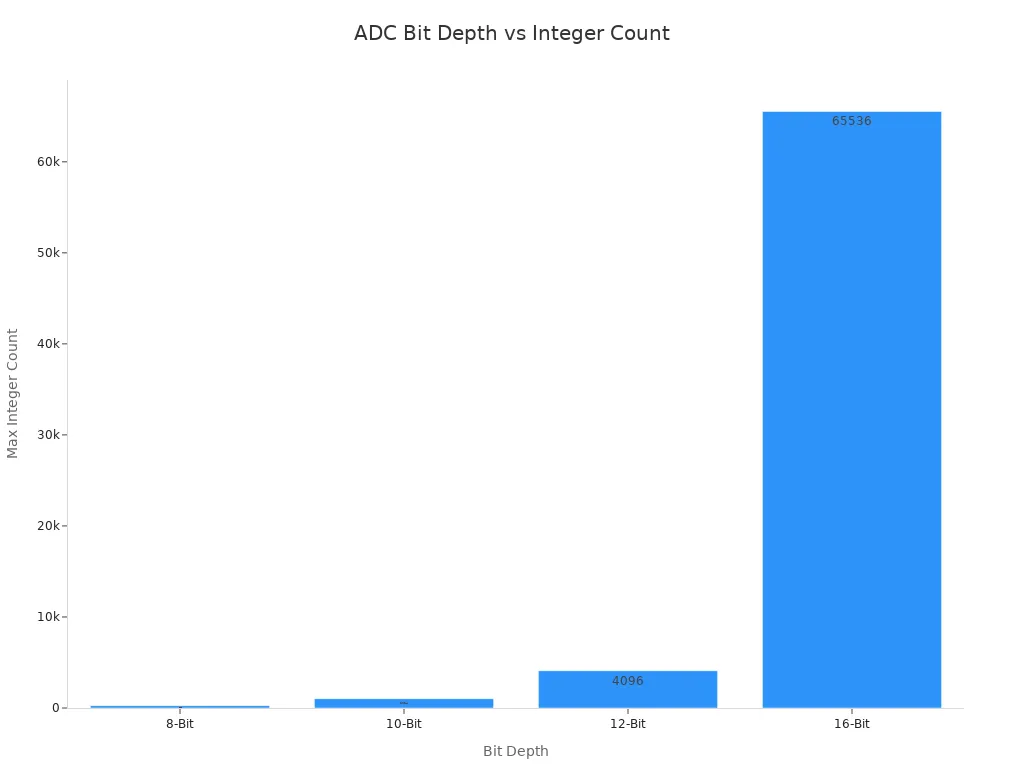
Bit depth sets number steps for your work.
| Bit Depth | Integer Count Range | Mathematical Formula |
|---|---|---|
| 8-Bit | 0 to 256 | 2^8 = 256 |
| 10-Bit | 0 to 1,024 | 2^10 = 1,024 |
| 12-Bit | 0 to 4,096 | 2^12 = 4,096 |
| 16-Bit | 0 to 65,536 | 2^16 = 65,536 |
Resolution and Raw Integer Count Representation
Resolution marks small power shifts you can see. High-resolution input channels split power ranges better.
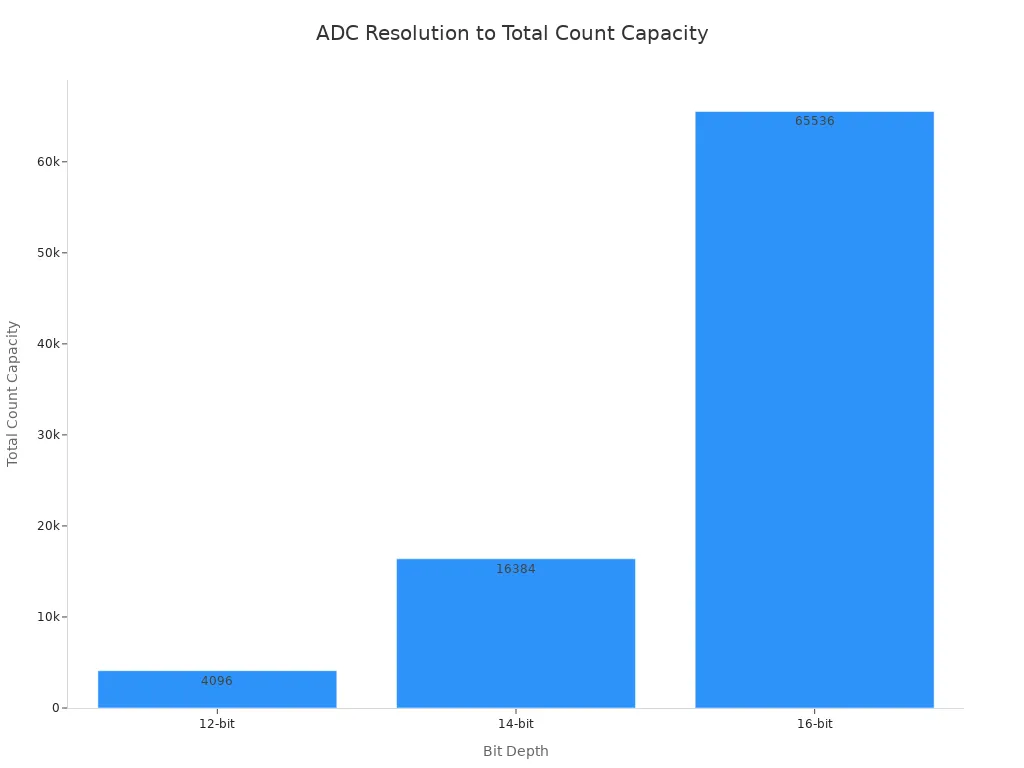
Bit size impacts exact work and overall control:
| Bit Depth | Total Count Capacity | Bipolar Configuration (Sign Bit) | Unipolar Precision (0–10V Range) |
|---|---|---|---|
| 12-bit | 4,096 counts | N/A | ~2.44 mV per step |
| 14-bit | 16,384 counts | N/A | ~0.61 mV per step |
| 16-bit | 65,536 counts | 32,768 counts (15-bit + sign) | ~0.15 mV per step |
Quantization error sets small limits for sensor data. Normal rounding error stays close to ±½ LSB. Upgrading from 12-bit to 16-bit helps greatly. It raises signal detail sixteen times over.
| Resolution Level / Error Impact | Effect on Process Control Accuracy & Stability | Mechanical & Operational Consequence |
|---|---|---|
| Low Resolution (High Quantization Error) | It makes rough step shifts. This harms PID precision. | It starts loop shakes. It wears out valves. |
| High Resolution (Reduced Quantization Error) | It permits small steps. PID runs very smoothly. | It aids tracking accuracy. It protects hard parts. |
Total accuracy relies on your adc input channel quality. Clean conversion stops useless hunts in main loops.
DAC Output Reconstruction for Actuator Control
An adc for industrial plc reads input data. A dac does the opposite job. A dac takes memory numbers to build voltage.
You send this signal to field parts. A dac guides fast motor drives and valves. Code puts numbers in storage. Then hardware builds the exact power value. Smooth changes depend on dac quality. Precise dac parts move valves without sharp jumps.
Industrial Analog Signal Standards and Wiring
Pick good wires for your plant setup. Field units link to your system boards. Safe setups keep your data steady and correct.
Current Loops Versus Voltage Signaling
Plants have big motors and heavy machines. They make strong power noise nearby. Check these two choices below:
| Characteristic | 0-10V Wiring | 4-20mA Loop |
|---|---|---|
| Noise Immunity | Low (susceptible to EMI pickup) | High (induced voltages do not alter loop current) |
| Line Loss | High (suffers from IR voltage drop across wire run) | None (transmitter maintains constant current despite cable length) |
| Max Cable Range | Short (~100–300 ft) | Extended (~1000–3000 ft) |
| Fault Detection | None (0V cannot distinguish 0% flow from broken line) | Built-in (0mA indicates a broken wire or open loop) |
Voltage signals fade across long wires. Current loops keep full power everywhere. A snapped line hits zero current. Your PLC finds this fault fast.
Two-Wire and Four-Wire Transmitter Connections
Sensors test real conditions inside your plant. They push real data to input boards. You can use two main designs:
| Feature / Characteristic | 2-Wire (Loop-Powered) Transmitter | 4-Wire (Externally Powered) Transmitter |
|---|---|---|
| Wiring Structure | Employs 2 conductors total, sharing both current and power transmission. | Uses 4 distinct conductors (2 dedicated to power, 2 dedicated to data). |
| Power Source & Delivery | Draws operating energy directly from the 4–20 mA current loop; 'steals' power to function. | Requires a completely separate AC or DC external power source. |
| Operational Power Capacity | Constrained power availability (must function within loop current limits). | High power capacity (can drive complex internal hardware, analytical tools, or heaters). |
| Electrical Isolation & Noise | Lacks output isolation due to shared wiring; offers standard noise immunity. | Delivers full electrical isolation between power and data circuits, eliminating ground loops and maximizing noise immunity. |
| Installation Complexity | Simple setup with minimal cabling requirements and lower overall cost. | Higher installation complexity and cost due to additional cabling demands. |
Two-wire units need fewer total cables. Four-wire units run heavy loads safely.
Grounding and Differential Wiring Best Practices
Safe wire steps shield weak signals:
-
Connect cable shields at panel ends only.
-
Cut field shield ends and cover them.
-
Use wrapped twin wires for signals.
-
Keep signal wires away from high power.
Balanced inputs remove matching noise across twin wires. Single-wire inputs share ground connections easily. They pick up extra signal noise. New input boards filter data very well. Good output drivers stop system mistakes.
PLC Memory Addressing and Register Mapping
New PLC units keep numbers in 16-bit registers. They save data inside image tables. Your sensors push readings straight to these storage spots. Old systems use set address lists. Modern controllers organize data using soft, loose formats. New analog boards turn real readings into numbers.
Tag-Based Addressing in Allen-Bradley Controllers
Allen-Bradley ControlLogix platforms group system modules using descriptive tags. They skip hard-coded numerical addresses. You check raw channel data using simple tag structures.
-
Tag Path Syntax: You read channel data directly using tags like
Local:3:I.Ch0Data. -
Data Types: Raw hardware readings store integers in
INTorDINTformats. -
Direct Logic Usage: You drop raw tag numbers right into compute function blocks.
Peripheral Memory Word Mapping in Siemens PLCs
Siemens controllers process physical values with direct memory maps. Main image buffers process digital bit logic. Peripheral memory word spaces handle continuous signals. Siemens PLC platforms update physical values during cycle runs.
-
Direct Hardware Interaction: The PLC reads field values instantly from outside hardware.
-
Access Limitations: You must move peripheral data in byte or word sizes.
-
Standard Word Notation: You write
PIWfor inputs andPQWfor outputs.
| Peripheral Address Type | Definition & Purpose | Operation Mechanics | Example Use Case |
|---|---|---|---|
| PIW | Reads input values directly from real-world field instruments | Transfers data immediately from physical hardware to user programs | Reading water tank levels from a sensor |
| PQW | Writes analog output signals directly to field execution devices | Outputs data directly to physical hardware | Setting speed on variable frequency motor drives |
Note: Add-on boards refresh raw counts faster using peripheral memory. This path skips normal image buffers.
Scaling Analog Signals in PLC Logic
Your main unit gets pure digital counts. Outer tools send these basic numbers. Change these counts to clear values. Use units like PSI or Celsius. Math changes simple counts to real measures.
Linear Scaling Formula and Engineering Units
Straight lines help find real physical values. You map counts into useful numbers.
-
Mechanism: Straight lines match raw data numbers. Use simple counts from 0 to 1023. These counts match actual temperature or pressure numbers.
-
Implementation: Main control units run built-in blocks. Blocks use low and high limits. Limits cover counts and final real ranges.
Math uses the standard Scale function:
SCP(Input, InputMin, InputMax, ScaledMin, ScaledMax, Output). For example, counts from 0 to 1023 map to 0 to 150 PSI with[SCP I:0.4 0 1023 0 150 N7:10].
Outer tools use current shifts to show errors. Clear rules set loop health check zones.
| Current Threshold | Operational Status | Loop Meaning | System Action |
|---|---|---|---|
| Between 4.0 and 20.0 mA | Standard Operation | Readings stay in safe limits | Scale main values normally |
| Between 3.8 and 4.0 mA | Lower Extended Range | Small drift or tiny negative number | Accept value; show low note |
| Between 20.0 and 20.5 mA | Upper Extended Range | Measured value slightly exceeds top limit | Accept value; show high note |
| 3.6 to 3.8 mA / 20.5 to 21.0 mA | Warning Zone | Non-critical internal fault detected | Show main warning without stop |
| At or below 3.6 mA | Severe Low Fault | Loop line cut or power gone | Mark bad; set safe state; send warning |
| At or above 21.0 mA | Severe High Fault | Short loop or high sensor break | Mark bad; set safe state; send warning |
To run basic fault safety, set limits at 3.6 mA and 21.0 mA. If units use other signal levels, set trigger points just past them. Small alerts show before full errors occur.
Some smart devices run self tests on power up. They test current low and high limits. Tests check total loop resistance and dynamic power across channels. Checking current states helps keep all tools fully accurate.
Ladder Logic Implementation Options
Different control systems use unique function blocks. Select exact tools based on your brand.
| PLC Platform | Scaling Instruction(s) | Functionality & Mathematical Approach |
|---|---|---|
| Allen-Bradley | SCP (Scale with Parameters) | Runs complete linear scaling inside one step using:EU_Value = ((Raw - Raw_Min) / (Raw_Max - Raw_Min)) * (EU_Max - EU_Min) + EU_Min |
| Siemens | NORM_X & SCALE_X | Employs two quick steps:1. NORM_X: Turns raw counts into a 0.0 to 1.0 decimal.2. SCALE_X: Maps decimal numbers into real target units. |
An Allen-Bradley unit scales data in one step. A Siemens unit uses two distinct steps. The NORM_X block changes raw counts to percentages. Next, the SCALE_X block maps percentages to final real numbers.
Structured Text Scaling Code Snippet
Write custom scaling logic using clear Structured Text code. Text lines handle unique numeric ranges easily.
FUNCTION_BLOCK FB_AnalogScale
VAR_INPUT
    RawInput    : INT;      // Analog input raw reading
    RawMin      : INT;      // Minimum raw limit
    RawMax      : INT;      // Maximum raw limit
    ScaleMin    : REAL;     // Minimum scaled engineering unit
    ScaleMax    : REAL;     // Maximum scaled engineering unit
END_VAR
VAR_OUTPUT
    ScaledValue : REAL;     // Calculated engineering output
END_VAR
VAR
    Slope       : REAL;
    Offset      : REAL;
END_VAR

// Compute m (slope) and b (offset)
Slope := (ScaleMax - ScaleMin) / INT_TO_REAL(RawMax - RawMin);
Offset := ScaleMin - (Slope * INT_TO_REAL(RawMin));

// Compute output via linear conversion equation y = mx + b
ScaledValue := (Slope * INT_TO_REAL(RawInput)) + Offset;

END_FUNCTION_BLOCK
Import this code into any open platform safely. Custom code gives full control over logic and errors.
Calibration, Drift, and Noise Mitigation
Fix your tools to keep accurate measures. Heat shifts parts out of place. This hurts your hardware over time.
| Industrial Field Condition | Impact on Analog IO / Sensors | Resulting Calibration Issue |
|---|---|---|
| Thermal Stress | Shifts inner part sizes | Changes basic resistance values |
| Component Aging | Hurts old circuit parts | Reduces total circuit stability |
| Environmental Contamination | Dirt and wet air | Blocks good signal flow |
| Mechanical Stress | Shakes and hard bumps | Scratches sensor wire joints |
| Electrical Interference | Long wires and noise | Adds bad reading errors |
Zero and Span Field Calibration Steps
Fix signal scale on current loops using five steps:
-
Pre-set the Potentiometer: Find zero and range screws. Turn both screws 20 turns right. Then turn them 10 turns left.
-
Apply Lower Range Value (LRV): Send zero push force now. Open low sides to clear air.
-
Calibrate Zero (4mA): Turn zero screws to hit 4mA.
-
Apply Upper Range Value (URV): Send full push force next.
-
Calibrate Span (20mA): Turn range screws to hit 20mA.
Temperature Drift and Offset Correction
Old sensors create wrong readings over time. Look at these common drift causes:
-
Field Instrumentation Wear: Wear breaks inner sensor tools.
-
Physical Line & Connection Degradation: Rust and water ruin long cables.
-
Internal Voltage Reference Shift: Heat changes inner board power.
-
Crystal Oscillator Aging: Old clocks lose exact time.
-
Transducer Mechanical Fatigue: Hard shakes bend sensor shapes.
Preventing Ground Loops and Interference
Protect input lines using clean wire setups. Bad ground loops make extra paths. Use isolated tools to stop extra currents. Ground shield ends at one panel only. Good wires guard dac output paths. Clean lines help PLCs control machines.
Hardware tools run factory machines all day.
An adc for industrial plc changes facts into numbers.
Your main unit processes logic fast.
It sends numbers out soon.
Next, a dac builds a real power signal.
You win with simple steps.
Check wires and tag paths.
Check math scaling rules.
Set zero and span values carefully.
Field checks stop system errors.
Use current loops in noisy plants.
| Characteristic | 0-10V Signal | 4-20mA Current Loop | ROI / Reliability Impact |
|---|---|---|---|
| Transmission Distance | Short range (< 30 meters) | Long range (> 300 meters) | Stops signal loss well |
| Broken Wire Detection | Hard to see | Fast check (0mA) | Cuts downtime and work |
Written by Jack Elliott from AIChipLink.
AIChipLink, one of the fastest-growing global independent electronic components distributors in the world, offers millions of products from thousands of manufacturers, and many of our in-stock parts is available to ship same day.
We mainly source and distribute integrated circuit (IC) products of brands such as Broadcom, Microchip, Texas Instruments, Infineon, NXP, Analog Devices, Qualcomm, Intel, etc., which are widely used in communication & network, telecom, industrial control, new energy and automotive electronics.
Empowered by AI, Linked to the Future. Get started on AIChipLink and submit your RFQ online today!
Frequently Asked Questions
What is the main job of an adc for industrial plc?
An adc for industrial plc changes physical signals to numbers. You use it to read data like temperature. It changes analog voltage to a digital input value.
How does a dac differ from an adc?
An adc processes incoming data. A dac converts numbers to physical signals. You send this output to field devices. These include valves and motor drives.
Why do signal modules require regular calibration routines?
Modules face aging and heat drift over time. You perform calibration to restore high accuracy. This maintenance aligns readings with true physical values.
What steps complete zero and span calibration?
First, you adjust the zero point at low levels. Next, you apply full load for span points. This two-step routine fixes errors. Calibration maintains system reliability.
How often should you check your plc input setup?
Inspect your plc input connections during scheduled care. Plants create noise and heat stress. Checks prevent bad readings and protect control loops.